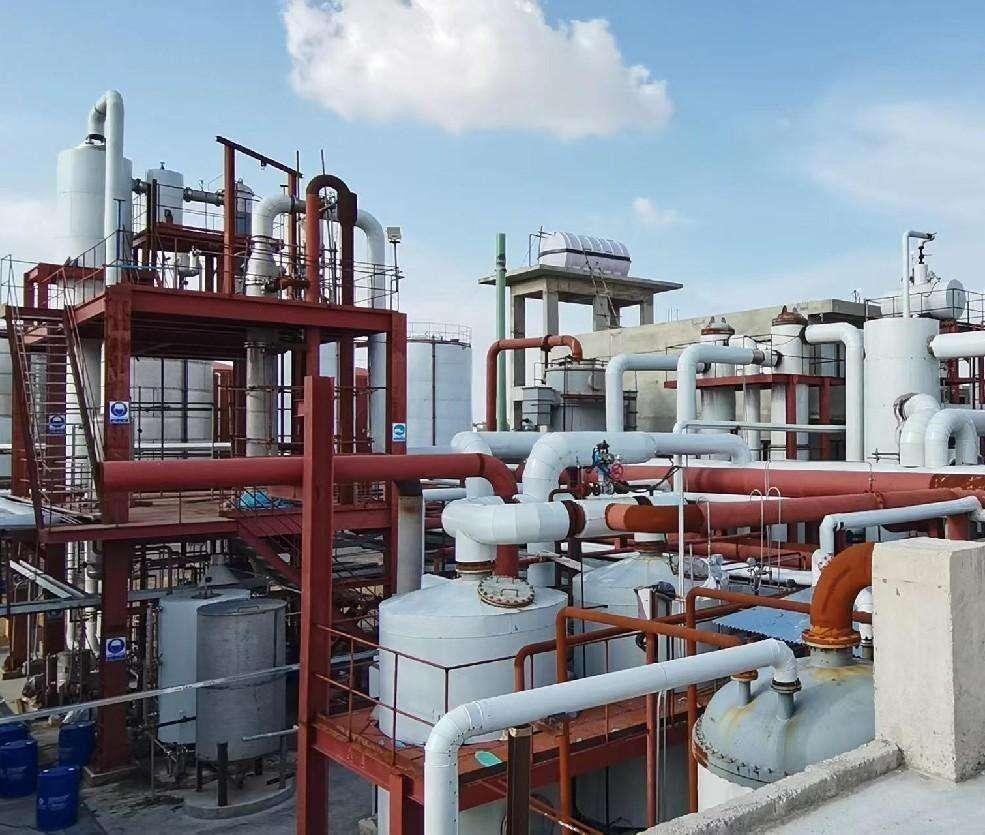
Turnkey industrial plants for the production of detergents, surfactants and sodium silicate.
Specialized technology in sulfonation and sulfation of LABSA, SLES, SLS and AOS. Advanced energy efficiency and sustainability systems, including heat recovery and emissions reduction.
Renewable energies, with integration of batteries and solar panels.
Modular and adaptable infrastructure, such as prefabricated warehouses, industrial racks and warehouses.
Optimized storage systems, with selective, drive-in, cantilever and automated racks.
High-precision mixing and packaging processes, using homogenizing, emulsifying and ripening equipment, as well as flexible and reliable automatic packaging solutions.
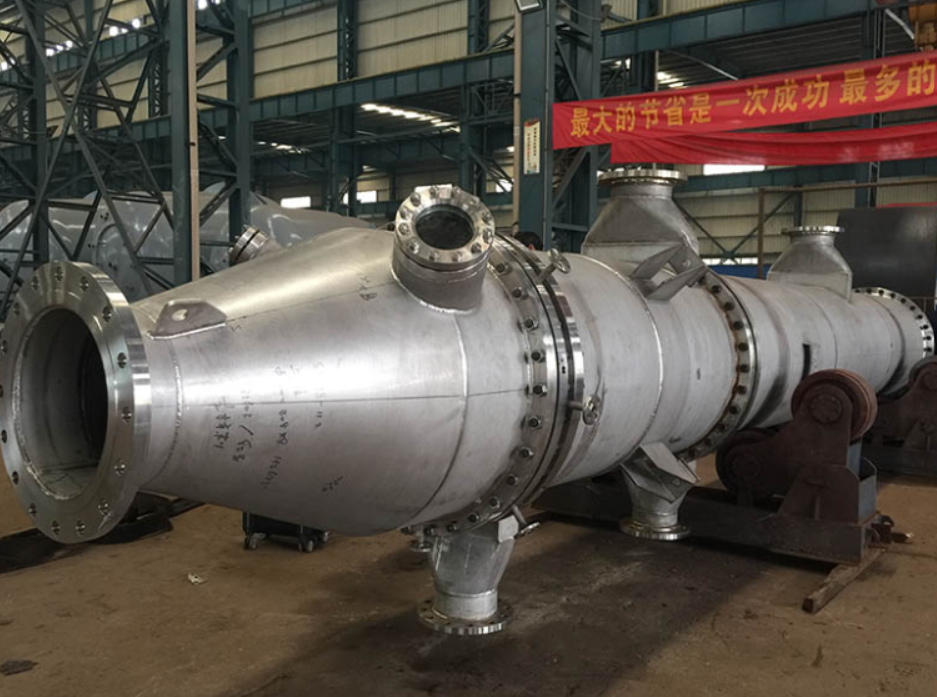
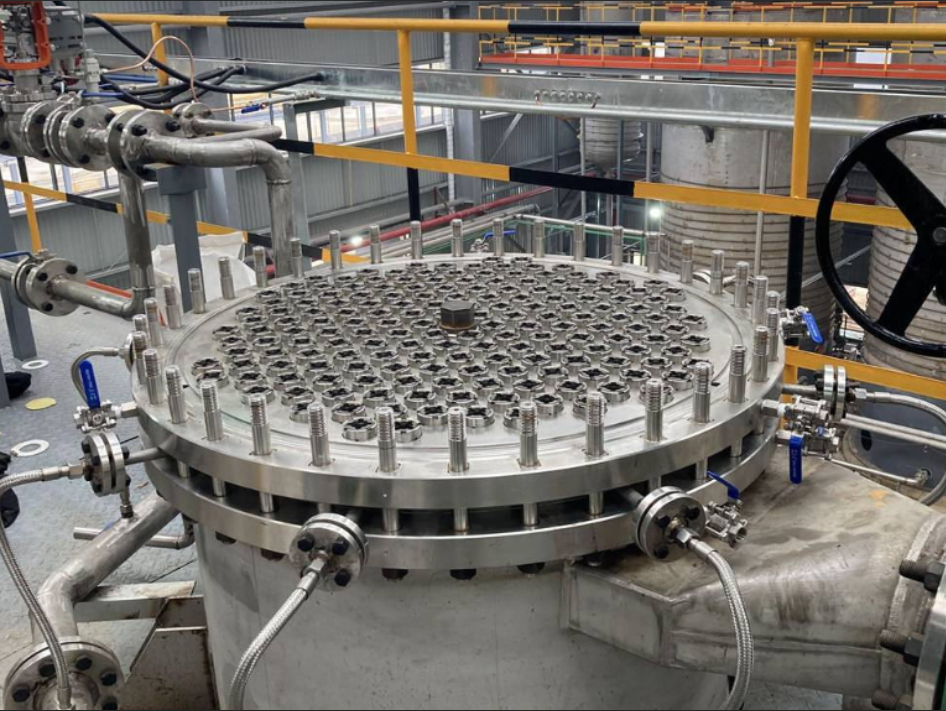
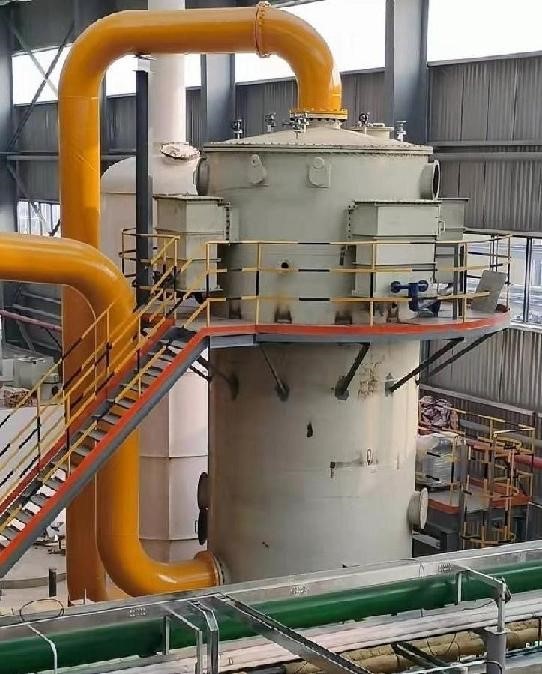
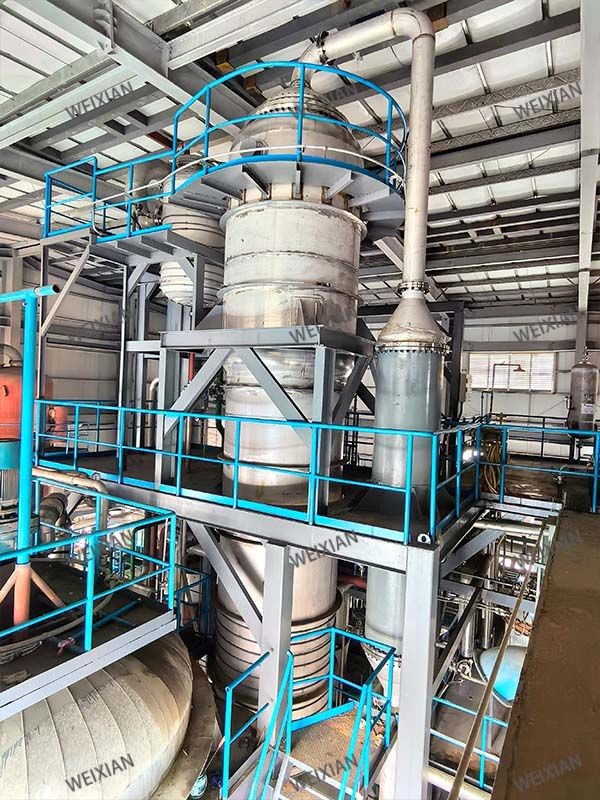
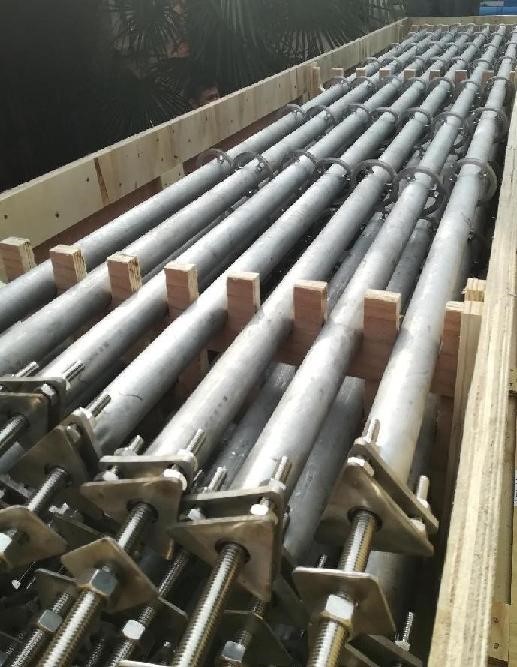
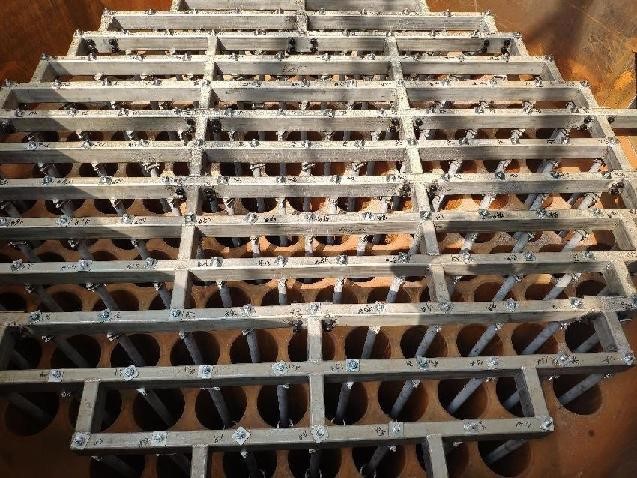
Success story: World's largest sulfonation reactor: 192 tubes, 8 TPH, executed by WEIXIAN
Introducing the world's largest sulfonation reactor: 192 tubes, 8 TPH - Designed by WEIXIAN!
Sulfonation/Sulfation Project - 180-tube WEIXIAN plant: 7.5 TPH of LABSA, 10 TPH of SLES and 15 TPH of AOS.
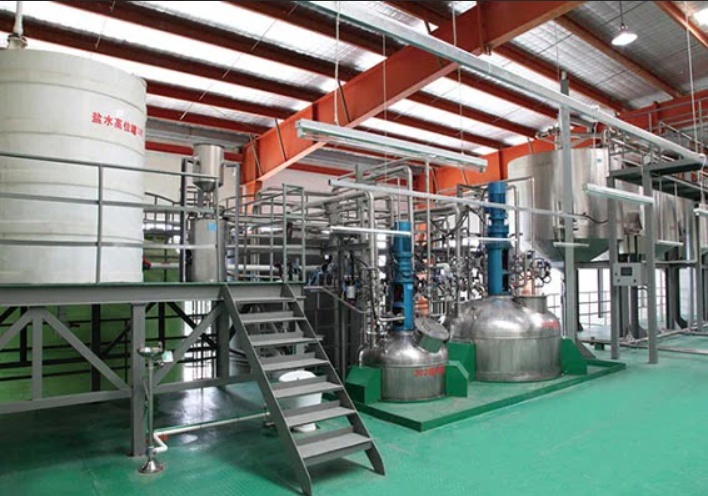
Success story: Unilever Sichuan, executed by Hangzhou Meibao
Success story: Unilever Sichuan, executed by Hangzhou Meibao